| Обновлено 2020-04-13 20:20:22 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
WIDIA | Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) |
|||||
1514 Каталог WIDIA 2017 Режущий инструмент Пластины Резцы Фрезы Сверла Метчики Стр.T146 |
|||||
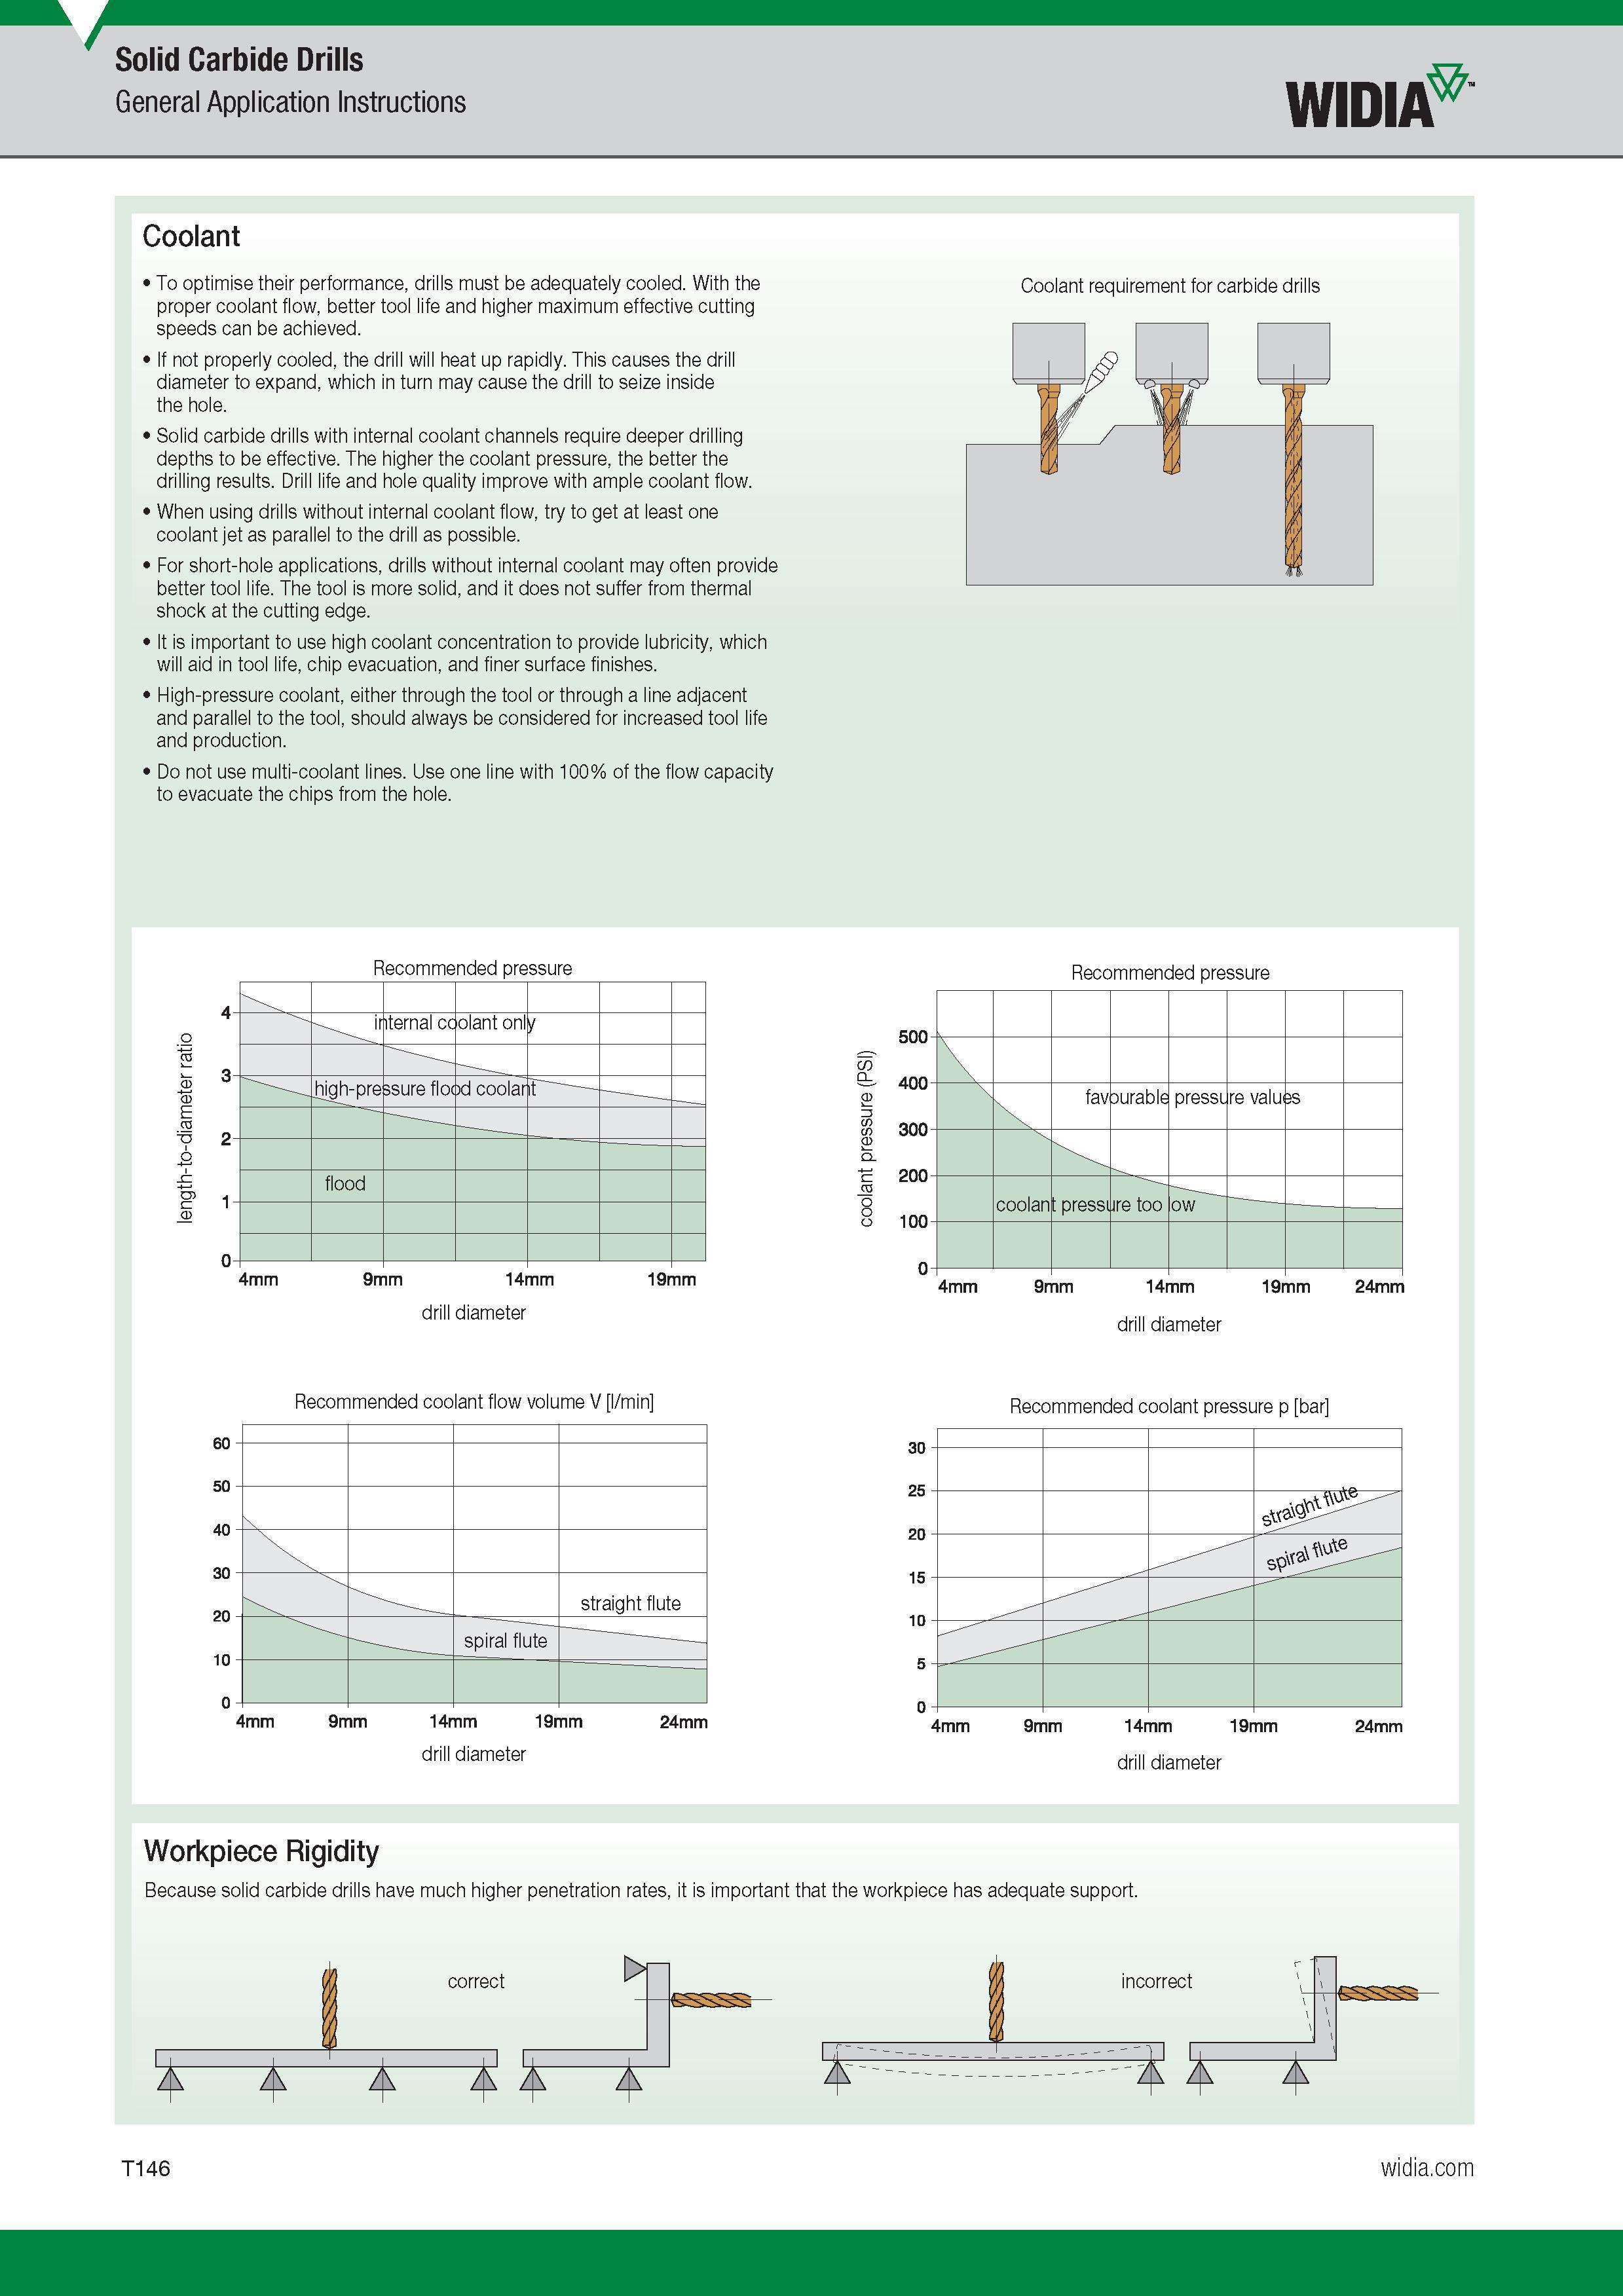
Каталог Widia 2017 Металлорежущий инструмент Стр. T146 1514 ENG Lab2u Solid Carbide Drills General Application Instructions Widia Coolant To optimise their performance, drills must be adequately cooled. With the proper coolant flow, better tool life and higher maximum effective cutting speeds can be achieved. If not properly cooled, the drill will heat up rapidly. This causes the drill diameter to expand, which in turn may cause the drill to seize inside the hole. Solid carbide drills with internal coolant channels require deeper drilling depths to be effective. The higher the coolant pressure, the better the drilling results. Drill life and hole quality improve with ample coolant flow. When using drills without internal coolant flow, try to get at least one coolant jet as parallel to the drill as possible. For short-hole applications, drills without internal coolant may often provide better tool life. The tool is more solid, and it does not suffer from thermal shock at the cutting edge. It is important to use high coolant concentration to provide lubricity, which will aid in tool life, chip evacuation, and finer surface finishes. High-pressure coolant, either through the tool or through a line adjacent and parallel to the tool, should always be considered for increased tool life and production. Do not use multi-coolant lines. Use one line with 100% of the flow capacity to evacuate the chips from the hole. Coolant requirement for carbide drills Recommended pressure in high-pre ternal ssure floo olant onl )d coolar y t flood 4mm 9mm 14mm 19mm drill diameter Recommended coolant flow volume V l/min drill diameter Recommended pressure drill diameter Recommended coolant pressure p bar drill diameter |
|||||
См.также / See also : |
|||||
Металлообработка Учебники и справочники / Metal Cutting Technology Technical Guide |
Особенности сверления металла / Drill a hole in metal |
||||
Токарная обработка металла / Basics of metal turning |
Фрезерование на фрезерном станке / Basics of milling |
||||
Нарезание резьбы метчиками / Tapping |
Развертывание отверстий и развертки по металлу / Reaming and reamer cutting tool |
||||
Расточка на токарном станке / Boring on a lathe |
Растачивание отверстий на расточном станке / Boring on a boring machine |
||||
| |
|||||
| WIDIA | |||||
| |
|||||
 Каталог WIDIA 2017 Металлорежущий инструмент (англ.яз. / ENG) (1972 страницы) |
|||||
 Каталог WIDIA 2018 Инструмент для металлообработки Новинки (106 страниц) |
 Каталог WIDIA 2017 Инструмент токарный для станков (668 страниц) |
 Каталог WIDIA 2017 Инструмент фрезерный монолитный (332 страницы) |
 Каталог WIDIA 2017 Инструмент для обработки отверстий (348 страниц) |
 Каталог WIDIA 2017 Фрезы резьбовые и метчики (122 страницы) |
|
 Каталог WIDIA 2016 Фрезы с режущими сменными пластинами (340 страниц) |
 Каталог WIDIA 2015 Токарный инструмент (382 страницы) |
 Каталог WIDIA 2014 Новый инструмент (422 страницы) |
 Каталог WIDIA 2012 Новый режущий инструмент и оснастка (470 страниц) |
 Каталог WIDIA 2011 Инструментальная оснастка (англ.яз. / ENG) (1190 страниц) |
 Каталог WIDIA 2010 Режущий осевой инструмент (614 страниц) |
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) | |||||
| |
|||||
 1511 |  1512 |  1513 |  1515 |  1516 |  1517 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
