| Обновлено 2020-04-13 20:20:22 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
WIDIA | Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) |
|||||
1484 Каталог WIDIA 2017 Режущий инструмент Пластины Резцы Фрезы Сверла Метчики Стр.T116 |
|||||
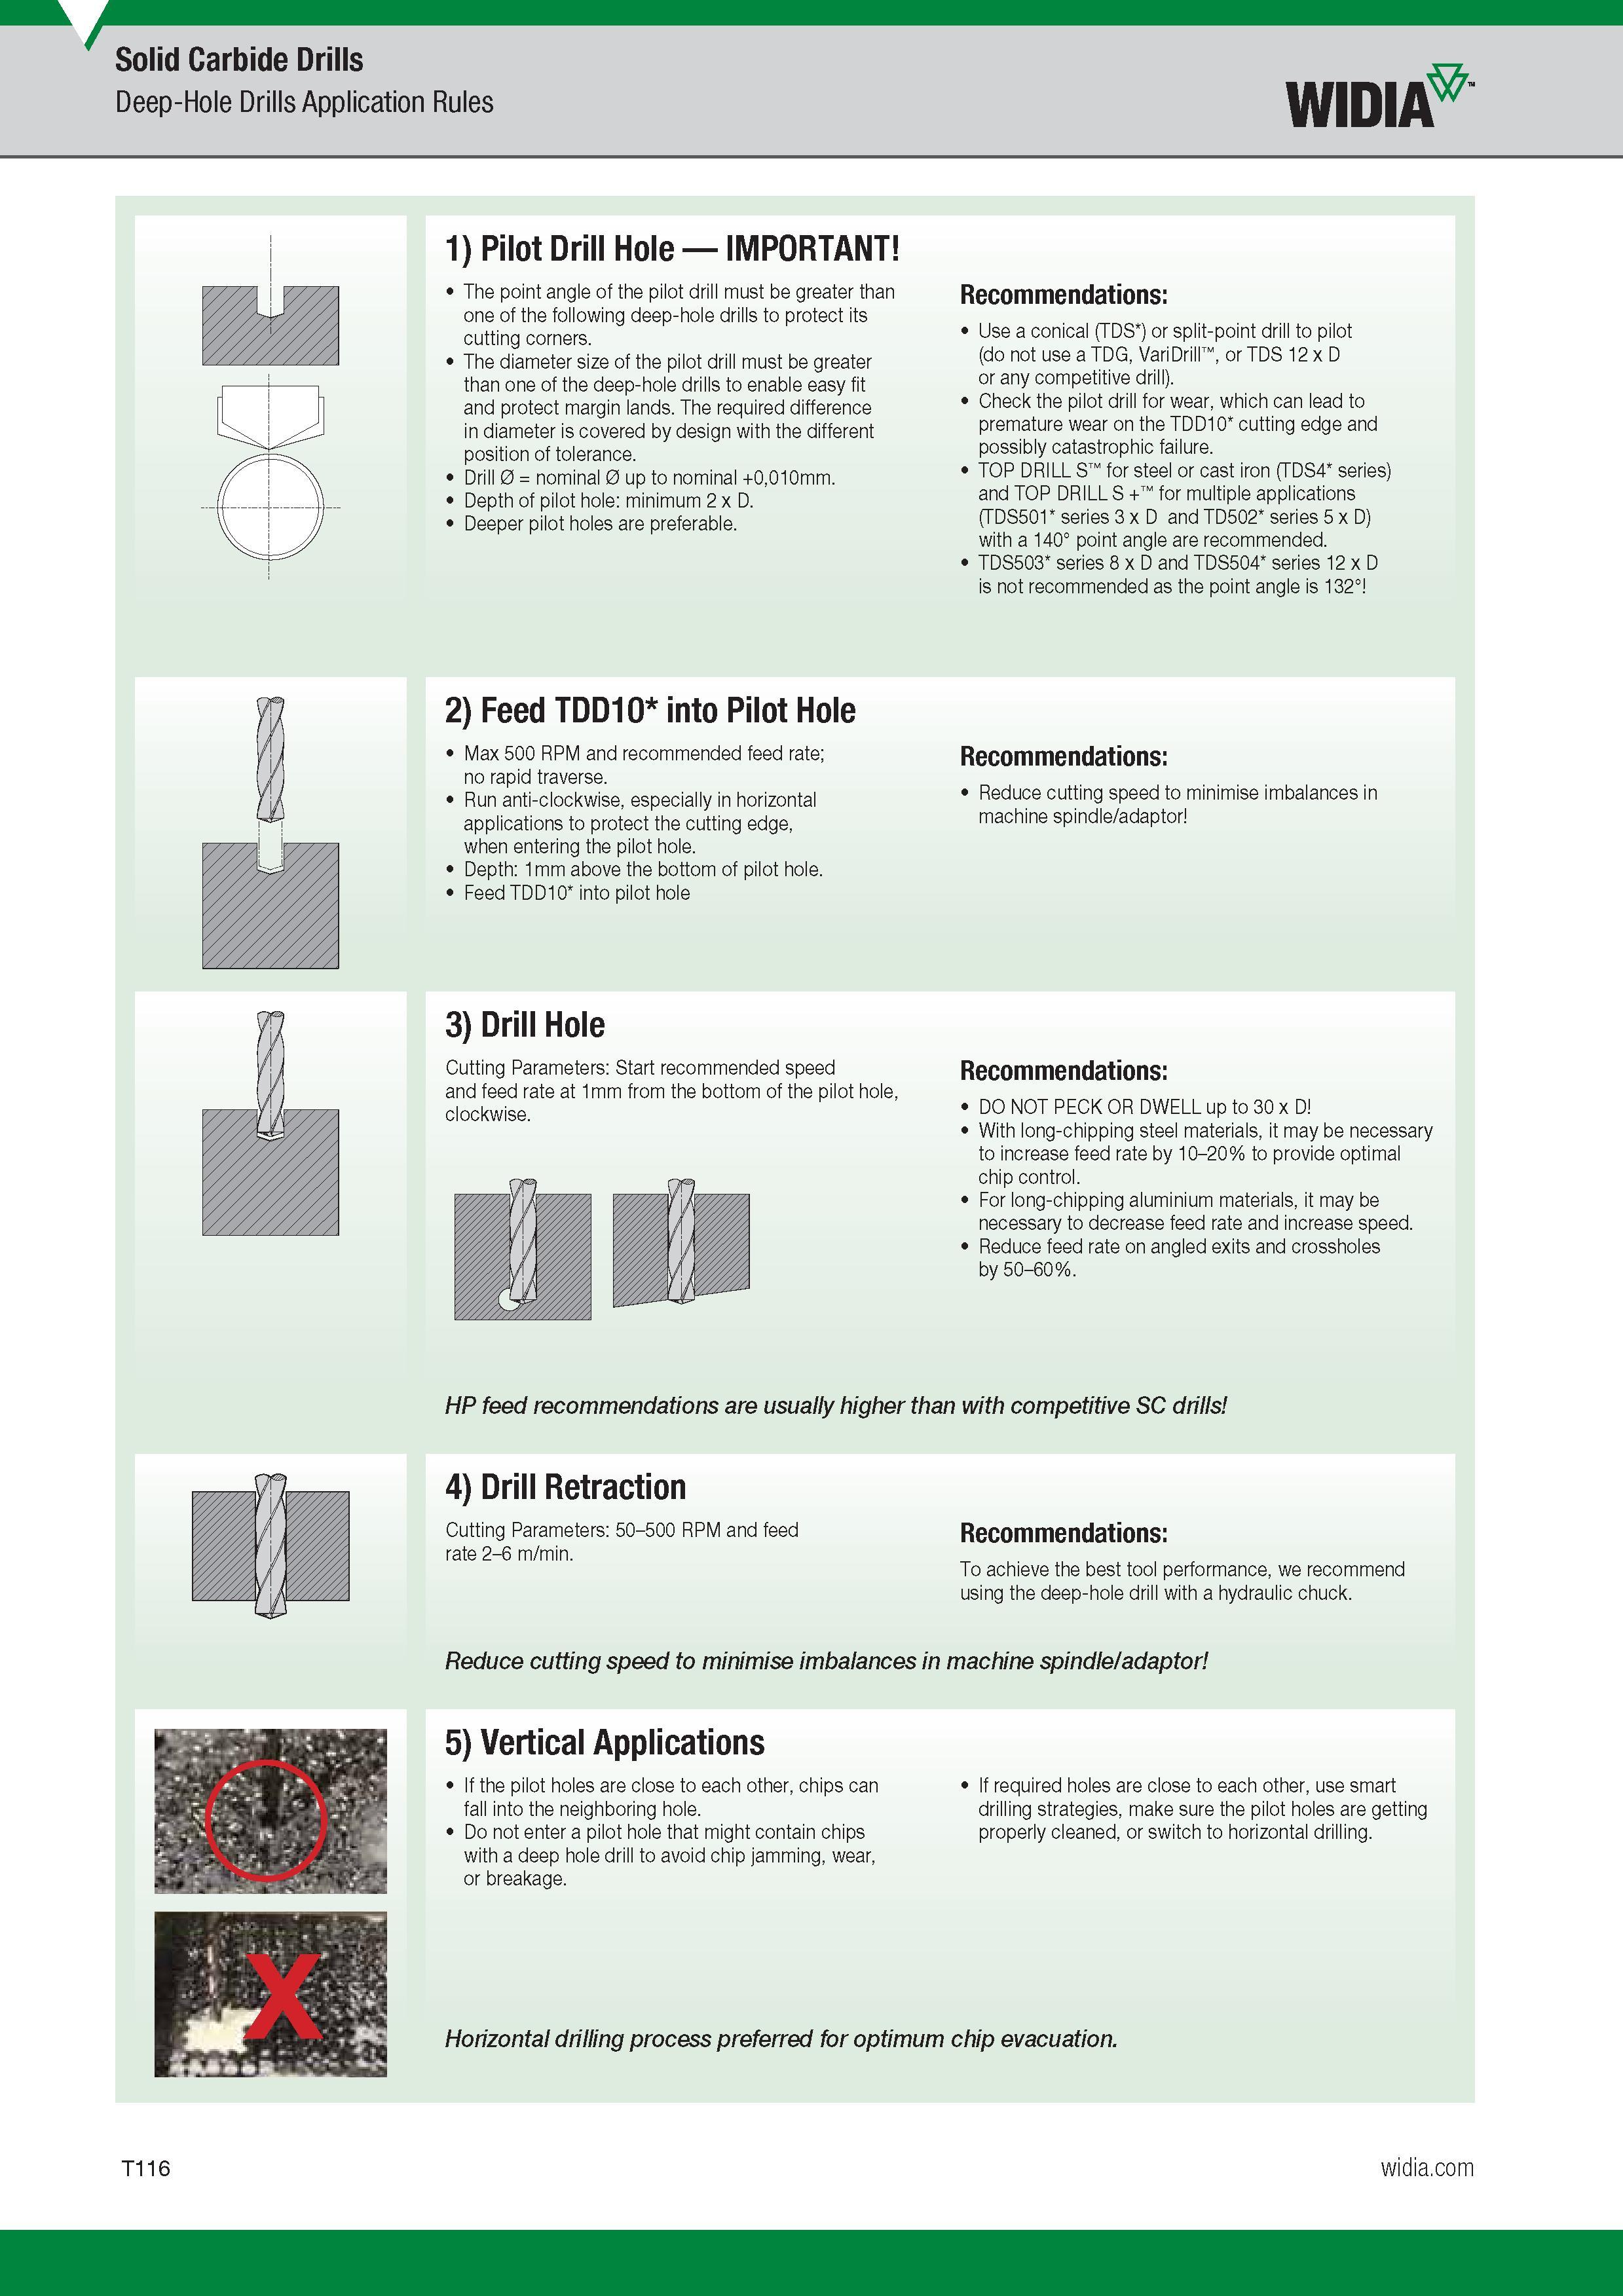
Каталог Widia 2017 Металлорежущий инструмент Стр. T116 1484 ENG Lab2u Solid Carbide Drills Deep-Hole Drills Application Rules Widia 1) Pilot Drill Hole IMPORTANT The point angle of the pilot drill must be greater than one of the following deep-hole drills to protect its cutting corners. The diameter size of the pilot drill must be greater than one of the deep-hole drills to enable easy fit and protect margin lands. The required difference in diameter is covered by design with the different position of tolerance. Drill 0 nominal 0 up to nominal +0,010mm. Depth of pilot hole minimum 2 x D. Deeper pilot holes are preferable. Recommendations Use a conical (TDS ) or split-point drill to pilot (do not use a TdG, VariDrill or TDS 12 x D or any competitive drill). Check the pilot drill for wear, which can lead to premature wear on the TDD10 cutting edge and possibly catastrophic failure. TOP DRILL S for steel or cast iron (TDS4 series) and TOP DRILL S + for multiple applications (TDS501 series 3 x D and TD502 series 5 x D) with a 140° point angle are recommended. TDS503 series 8 x D and TDS504 series 12 x D is not recommended as the point angle is 132° 2) Feed TDD10 into Pilot Hole Max 500 RPM and recommended feed rate; no rapid traverse. Run anti-clockwise, especially in horizontal applications to protect the cutting edge, when entering the pilot hole. Depth 1mm above the bottom of pilot hole. Feed TDD10 into pilot hole Recommendations Reduce cutting speed to minimise imbalances in machine spindle/adaptor 3) Drill Hole Cutting Parameters Start recommended speed and feed rate at 1mm from the bottom of the pilot hole, clockwise. Recommendations DO NOT PECK OR DWELL up to 30 x D With long-chipping steel materials, it may be necessary to increase feed rate by 10-20% to provide optimal chip control. For long-chipping aluminium materials, it may be necessary to decrease feed rate and increase speed. Reduce feed rate on angled exits and crossholes by 50-60%. HP feed recommendations are usually higher than with competitive SC drills 5) Vertical Applications If the pilot holes are close to each other, chips can fall into the neighboring hole. Do not enter a pilot hole that might contain chips with a deep hole drill to avoid chip jamming, wear, or breakage. I f required holes are close to each other, use smart drilling strategies, make sure the pilot holes are getting properly cleaned, or switch to horizontal drilling. Horizontal drilling process preferred for optimum chip evacuation. |
|||||
См.также / See also : |
|||||
Металлообработка Учебники и справочники / Metal Cutting Technology Technical Guide |
Особенности сверления металла / Drill a hole in metal |
||||
Токарная обработка металла / Basics of metal turning |
Фрезерование на фрезерном станке / Basics of milling |
||||
Нарезание резьбы метчиками / Tapping |
Развертывание отверстий и развертки по металлу / Reaming and reamer cutting tool |
||||
Расточка на токарном станке / Boring on a lathe |
Растачивание отверстий на расточном станке / Boring on a boring machine |
||||
| |
|||||
| WIDIA | |||||
| |
|||||
 Каталог WIDIA 2017 Металлорежущий инструмент (англ.яз. / ENG) (1972 страницы) |
|||||
 Каталог WIDIA 2018 Инструмент для металлообработки Новинки (106 страниц) |
 Каталог WIDIA 2017 Инструмент токарный для станков (668 страниц) |
 Каталог WIDIA 2017 Инструмент фрезерный монолитный (332 страницы) |
 Каталог WIDIA 2017 Инструмент для обработки отверстий (348 страниц) |
 Каталог WIDIA 2017 Фрезы резьбовые и метчики (122 страницы) |
|
 Каталог WIDIA 2016 Фрезы с режущими сменными пластинами (340 страниц) |
 Каталог WIDIA 2015 Токарный инструмент (382 страницы) |
 Каталог WIDIA 2014 Новый инструмент (422 страницы) |
 Каталог WIDIA 2012 Новый режущий инструмент и оснастка (470 страниц) |
 Каталог WIDIA 2011 Инструментальная оснастка (англ.яз. / ENG) (1190 страниц) |
 Каталог WIDIA 2010 Режущий осевой инструмент (614 страниц) |
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) | |||||
| |
|||||
 1481 |  1482 |  1483 |  1485 |  1486 |  1487 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
