| Обновлено 2020-04-11 09:47:32 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
MITSUBISHI | Каталог MITSUBISHI 2018 Инструмент режущий (Всего 2040 стр.) |
|||||
Токарные канавочные резцы Mitsubishi для наружного и внутреннего точения GROOVING581 Каталог MITSUBISHI 2018 Инструмент режущий Пластины Фрезы Сверла Резцы Державки Стр.581 |
|||||
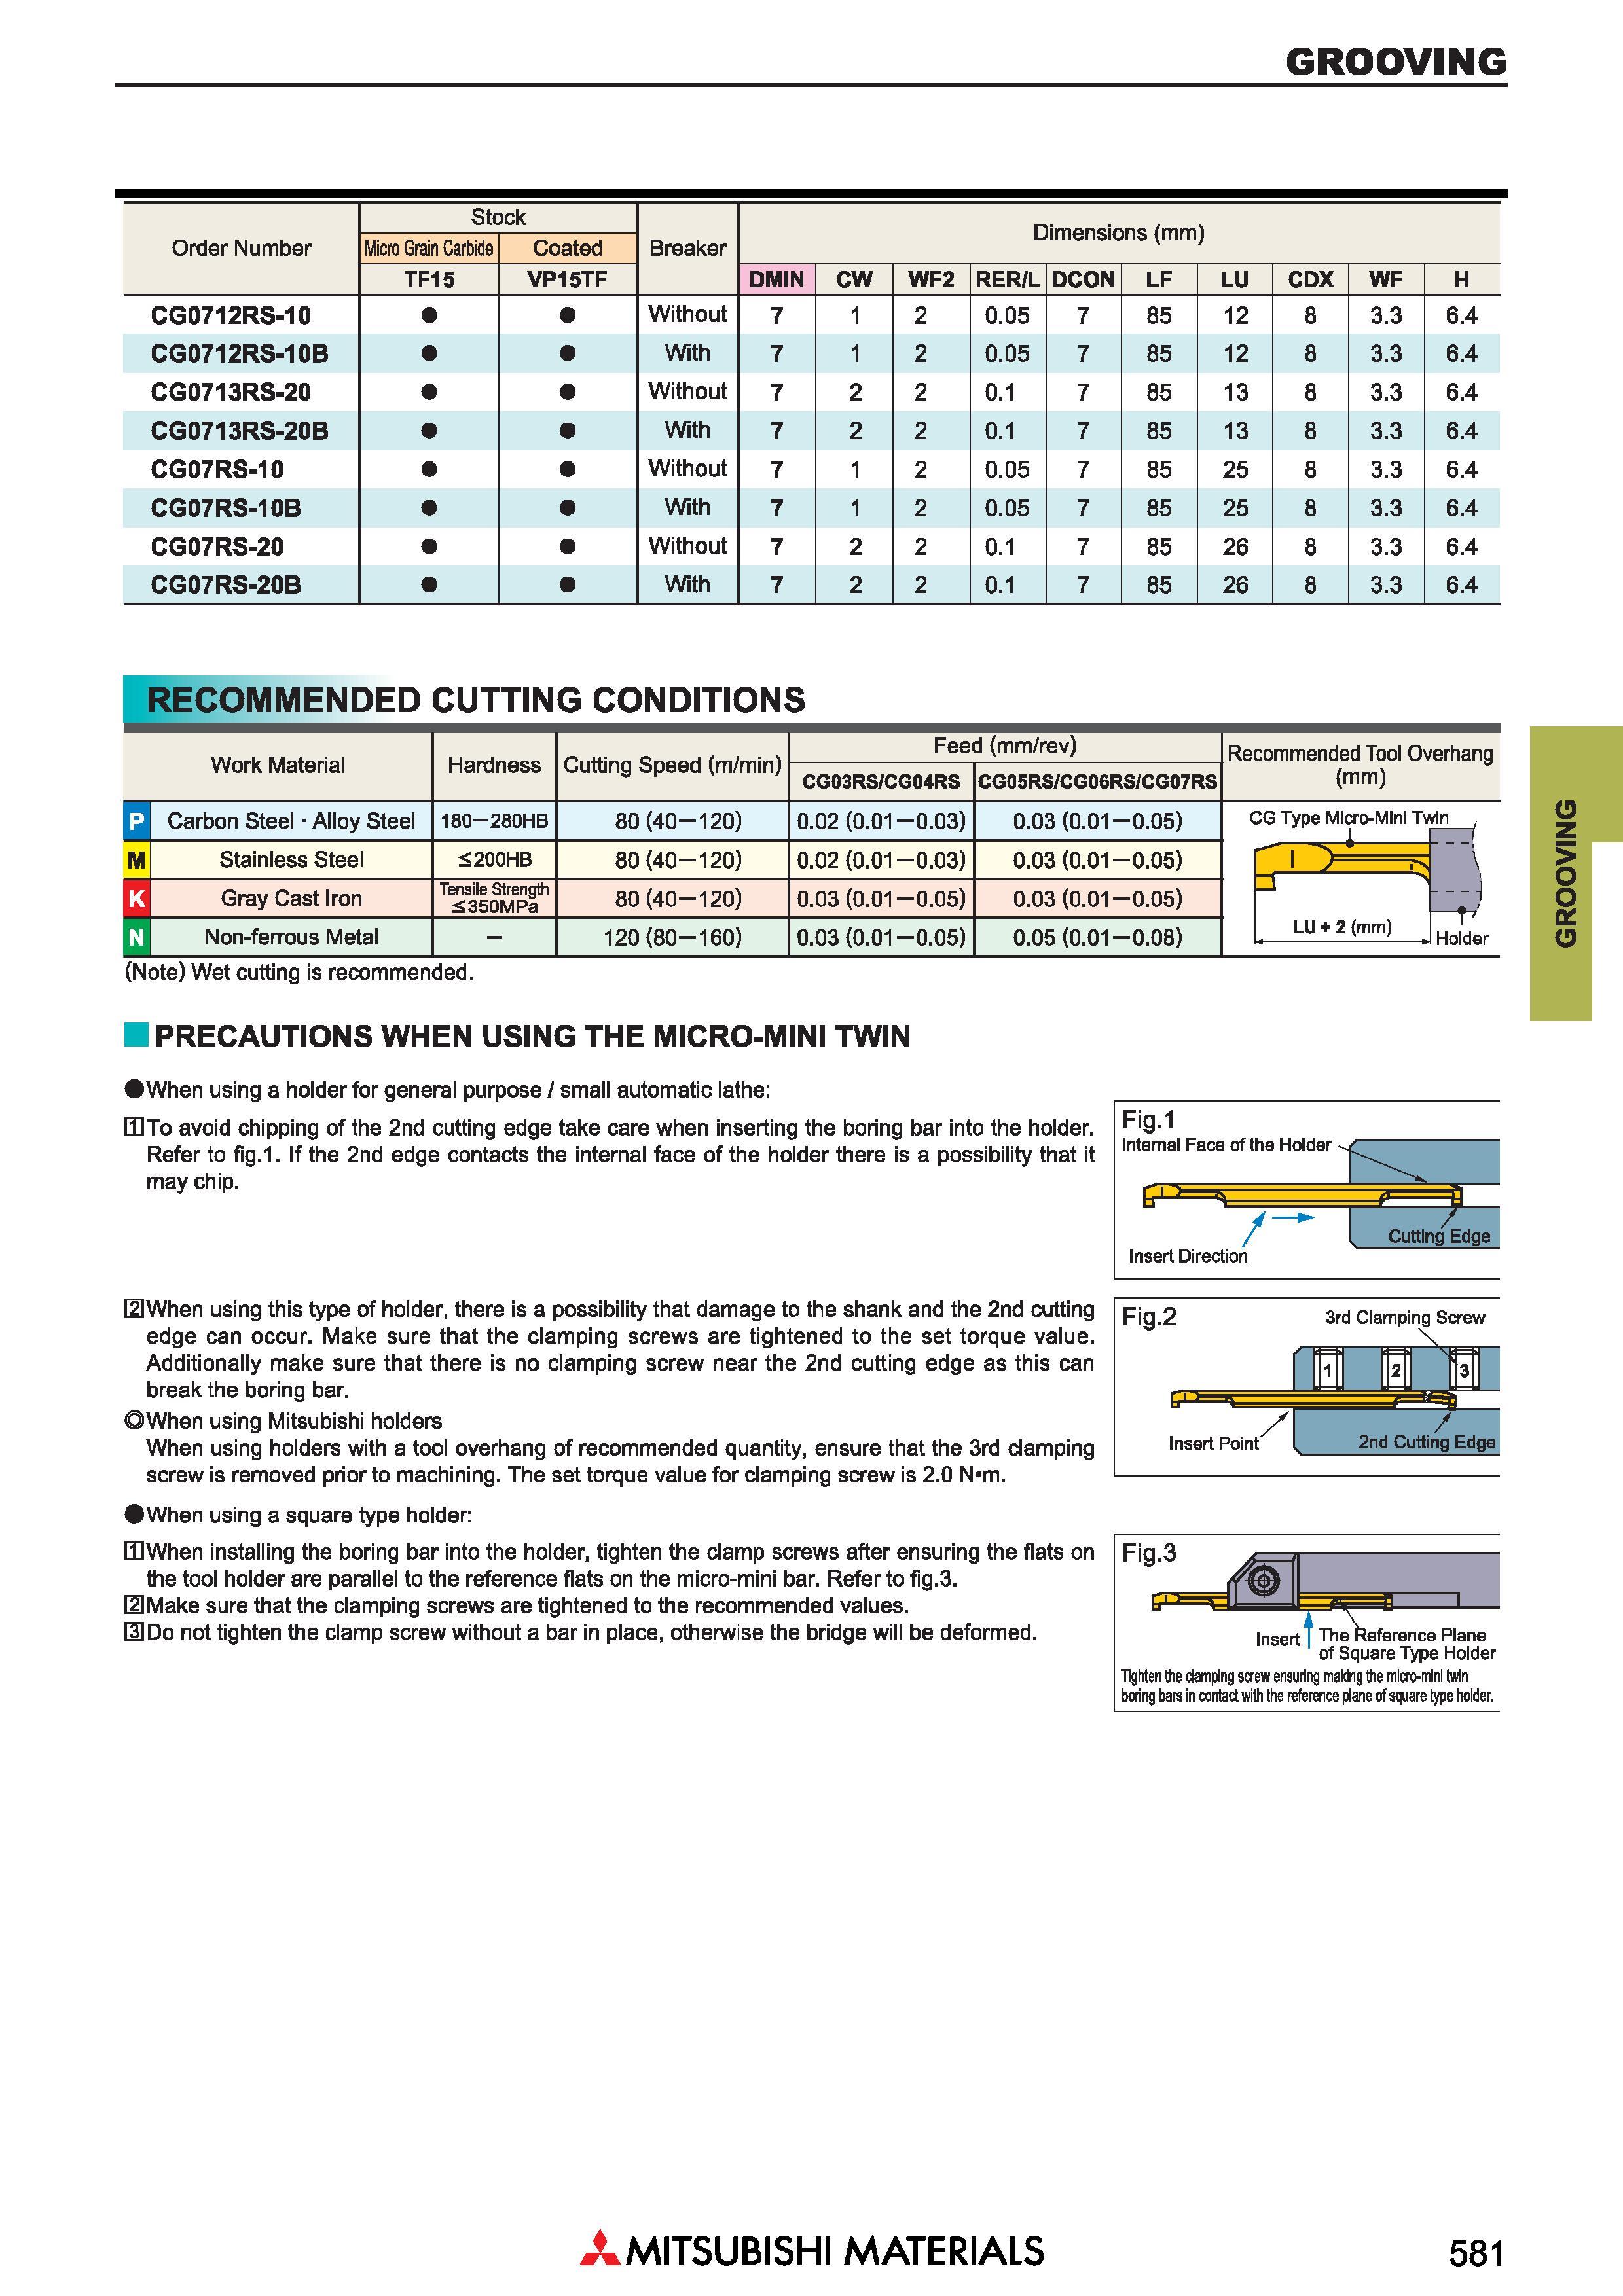
Токарные канавочные резцы Mitsubishi для наружного и внутреннего точения GROOVING Токарные канавочные резцы Mitsubishi для наружного и внутреннего точения GROOVING _ Обозначение Order Number Stock Breaker Размеры в мм Dimensions (mm) Micro Grain Carbide Coated TF15 VP15TF DMIN CW WF2 RER/L DCON LF LU CDX WF H CG0712RS-10 Without 7 1 2 0.05 7 85 12 8 3.3 6.4 CG0712RS-10B With 7 1 2 0.05 7 85 12 8 3.3 6.4 CG0713RS-20 Without 7 2 2 0.1 7 85 13 8 3.3 6.4 CG0713RS-20B With 7 2 2 0.1 7 85 13 8 3.3 6.4 CG07RS-10 Without 7 1 2 0.05 7 85 25 8 3.3 6.4 CG07RS-10B With 7 1 2 0.05 7 85 25 8 3.3 6.4 CG07RS-20 Without 7 2 2 0.1 7 85 26 8 3.3 6.4 CG07RS-20B With 7 2 2 0.1 7 85 26 8 3.3 6.4 Рекомендуемые режимы резания при обработке на станке RECOMMENDED CUTTING CONDITIONS Обрабатываемые материалы Work Material Carbon Steel Alloy Steel Hardness Скорость резания (м/мин) Cutting Speed (m/min) Подача (мм/оборот) Feed (mm/rev) CG03RS/CG04RS CG0SRS/CG06RS/CG07RS Recommended Tool Overhang (mm) 180 280HB 80(40-120) 0.02 (0.01 -0.03) 0.03 (0.01-0.05) M I Stainless Steel 200HB 80(40-120) 0.02 (0.01-0.03) 0.03 (0.01-0.05) CG Type Micro-Mini Twin Tj±= Gray Cast Iron Tensile Strength i350MPa 80(40-120) 0.03 (0.01 -0.05) 0.03 (0.01-0.05) Non-ferrous Metal 120 (80-160) 0.03 (0.01 -0.05) 0.05 (0.01-0.08) LU + 2 (mm) \ i Holder (Note) Wet cutting is recommended. PRECAUTIONS WHEN USING THE MICRO-MINI TWIN When using a holder for general purpose / small automatic lathe: fflTo avoid chipping of the 2nd cutting edge take care when inserting the boring bar into the holder. Refer to fig.1. If the 2nd edge contacts the internal face of the holder there is a possibility that it may chip. ElWhen using this type of holder, there is a possibility that damage to the shank and the 2nd cutting edge can occur. Make sure that the clamping screws are tightened to the set torque value. Additionally make sure that there is no clamping screw near the 2nd cutting edge as this can break the boring bar. When using Mitsubishi holders When using holders with a tool overhang of recommended quantity, ensure that the 3rd clamping screw is removed prior to machining. The set torque value for clamping screw is 2.0 N m. When using a square type holder: When installing the boring bar into the holder, tighten the clamp screws after ensuring the flats on the tool holder are parallel to the reference flats on the micro-mini bar. Refer to fig.3. El Make sure that the clamping screws are tightened to the recommended values. HI Do not tighten the clamp screw without a bar in place, otherwise the bridge will be deformed. Fig.1 Internal Face of the Holder Insert Direction Fig.2 3rd Clamping Screw 1 2 3jj Insert Point' / 2nd Cutting Edge Fig.3 £ Insert The Reference Plane of Square Type Holder Tighten the damping screw ensuring making the micro-mini twin in contact with the reference plane of square type holder. Mitsubishi Materials 581 GROOVING |
|||||
См.также / See also : |
|||||
Соотношение твердостей Таблица / Hardness equivalent table |
Аналоги марок стали / Workpiece material conversion table |
||||
Отклонение размера детали / Fit tolerance table |
Перевод оборотов в скорость / Surface speed to RPM conversion |
||||
Диаметр под резьбу / Tap drill sizes |
Виды резьбы в машиностроении / Thread types and applications |
||||
Дюймы в мм Таблица / Inches to mm Conversion table |
Современные инструментальные материалы / Cutting tool materials |
||||
| |
|||||
| MITSUBISHI | |||||
| |
|||||
 Каталог MITSUBISHI 2018 Инструмент режущий (англ.яз / ENG) (2040 страниц) |
 Каталог MITSUBISHI 2017 Новинки металлорежущего инструмента 17.1 (250 страниц) |
 Каталог MITSUBISHI 2016 Вращающийся и токарный режущий инструмент (1412 страниц) |
 Каталог MITSUBISHI 2016 Металлорежущий инструмент для мехобработки (англ.яз / ENG) (1636 страниц) |
 Каталог MITSUBISHI 2015 Токарный и вращающийся инструмент (англ.яз / ENG) (1672 страницы) |
 Каталог MITSUBISHI 2015 Новый режущий инструмент 15.2 (308 страниц) |
 Каталог MITSUBISHI 2015 Сверла для обработки отверстий в металле (англ.яз / ENG) (226 страниц) |
 Каталог MITSUBISHI 2014 Металлорежущий инструмент (1352 страницы) |
 Каталог MITSUBISHI 2014 Новый металлорежущий инструмент 14.2 (164 страницы) |
 Каталог MITSUBISHI 2013 Металлорежущий инструмент (1232 страницы) |
 Каталог MITSUBISHI 2010 Режущий инструмент и системы (1348 страницы) |
 Каталог MITSUBISHI 2007 Металлорежущий инструмент и системы (1085 страниц) |
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог MITSUBISHI 2018 Инструмент режущий (Всего 2040 стр.) | |||||
| |
|||||
 578 |  579 |  580 |  582 |  583 |  584 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
