| Обновлено 2020-04-13 20:20:03 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
WIDIA | Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) |
|||||
|
595 Каталог WIDIA 2017 Режущий инструмент Пластины Резцы Фрезы Сверла Метчики Стр.E131 |
|||||

Improve chip control Adjust feed rate up or down to accommodate chip formation Use a 0° or smallest lead available Use ample amounts of well-directImprove chip control Adjust feed rate up or down to accommodate chip formation. Use a 0° or smallest lead available. Use ample amounts of well-directed coolant (see Figure A). Maintain sharp cutting edge and corners. Improve flatness of cut-off surfaces Maintain 90° position (perpendicular alignment) between cut-off tool and workpiece. For low to moderate speed (sfpm), use Separator F2. For moderate to high speed (sfpm), use Separator S2 or X2. Use strongest toolholder system possible. Use 0° lead angle inserts when possible. If lead angle inserts are needed, reduce the feed rate. Check for minimum overhang of holder and blade. Set up for minimum workpiece overhang (distance out of chuck). Reduce feed rate. Maintain sharp edge and corners on cut-off insert. Increase speed (RPM). Use ample amounts of well-directed coolant (see Figure A). Maintain proper tool centre height 0-0,1mm above centre (see Figure B). Improve surface finish For low to moderate speed (sfpm), use Separator F2. For moderate to high speed (sfpm), use Separator S2 or X2. Avoid overly aggressive chip control. Increase speed. Reduce lead angle and feed rate. Determine if corner radius is too large or small. Use a coated grade . Use coolant (see Figure A). Figure A Coolant on cut-off tool Preferred method of applying coolant Figure B Minimise edge chipping Check to see if tool is significantly above or below centre. Reduce feed prior to part drop-off. Use Separator S2 or X2. Choose the proper speed associated with the insert grade used. Call Technical Support to see if a larger hone size is needed. Eliminate chatter. Avoid chip re-cutting. Check for these part and machine problems - Slide is loose. - Slide travel is irregular. - Bar/tube I.D. and/or O.D. is out of round. - Bar/tube is bent. - Thin wall collapses (deforms) in the cut. - Part is unstable. - Cut-off through unturned stock. - Excessive tool overhang. - Bent or partly attached flash ring. Separator Widia Technical Recommendations Separator Cut-Off System |
|||||
См.также / See also : |
|||||
Соотношение твердостей Таблица / Hardness equivalent table |
Аналоги марок стали / Workpiece material conversion table |
||||
Отклонение размера детали / Fit tolerance table |
Перевод оборотов в скорость / Surface speed to RPM conversion |
||||
Диаметр под резьбу / Tap drill sizes |
Виды резьбы в машиностроении / Thread types and applications |
||||
Дюймы в мм Таблица / Inches to mm Conversion table |
Современные инструментальные материалы / Cutting tool materials |
||||
| |
|||||
| WIDIA | |||||
| |
|||||
 Каталог WIDIA 2017 Металлорежущий инструмент (англ.яз. / ENG) (1972 страницы) |
|||||
 Каталог WIDIA 2018 Инструмент для металлообработки Новинки (106 страниц) |
 Каталог WIDIA 2017 Инструмент токарный для станков (668 страниц) |
 Каталог WIDIA 2017 Инструмент фрезерный монолитный (332 страницы) |
 Каталог WIDIA 2017 Инструмент для обработки отверстий (348 страниц) |
 Каталог WIDIA 2017 Фрезы резьбовые и метчики (122 страницы) |
|
 Каталог WIDIA 2016 Фрезы с режущими сменными пластинами (340 страниц) |
 Каталог WIDIA 2015 Токарный инструмент (382 страницы) |
 Каталог WIDIA 2014 Новый инструмент (422 страницы) |
 Каталог WIDIA 2012 Новый режущий инструмент и оснастка (470 страниц) |
 Каталог WIDIA 2011 Инструментальная оснастка (англ.яз. / ENG) (1190 страниц) |
 Каталог WIDIA 2010 Режущий осевой инструмент (614 страниц) |
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) | |||||
| |
|||||
 592 |  593 | 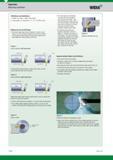 594 |  596 |  597 |  598 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
