| Обновлено 2020-04-13 20:20:03 |
|
Режущий инструмент, инструментальная оснастка и приспособления / Cutting tools, tooling system and workholding
WIDIA | Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) |
|||||
|
685 Каталог WIDIA 2017 Режущий инструмент Пластины Резцы Фрезы Сверла Метчики Стр.F87 |
|||||
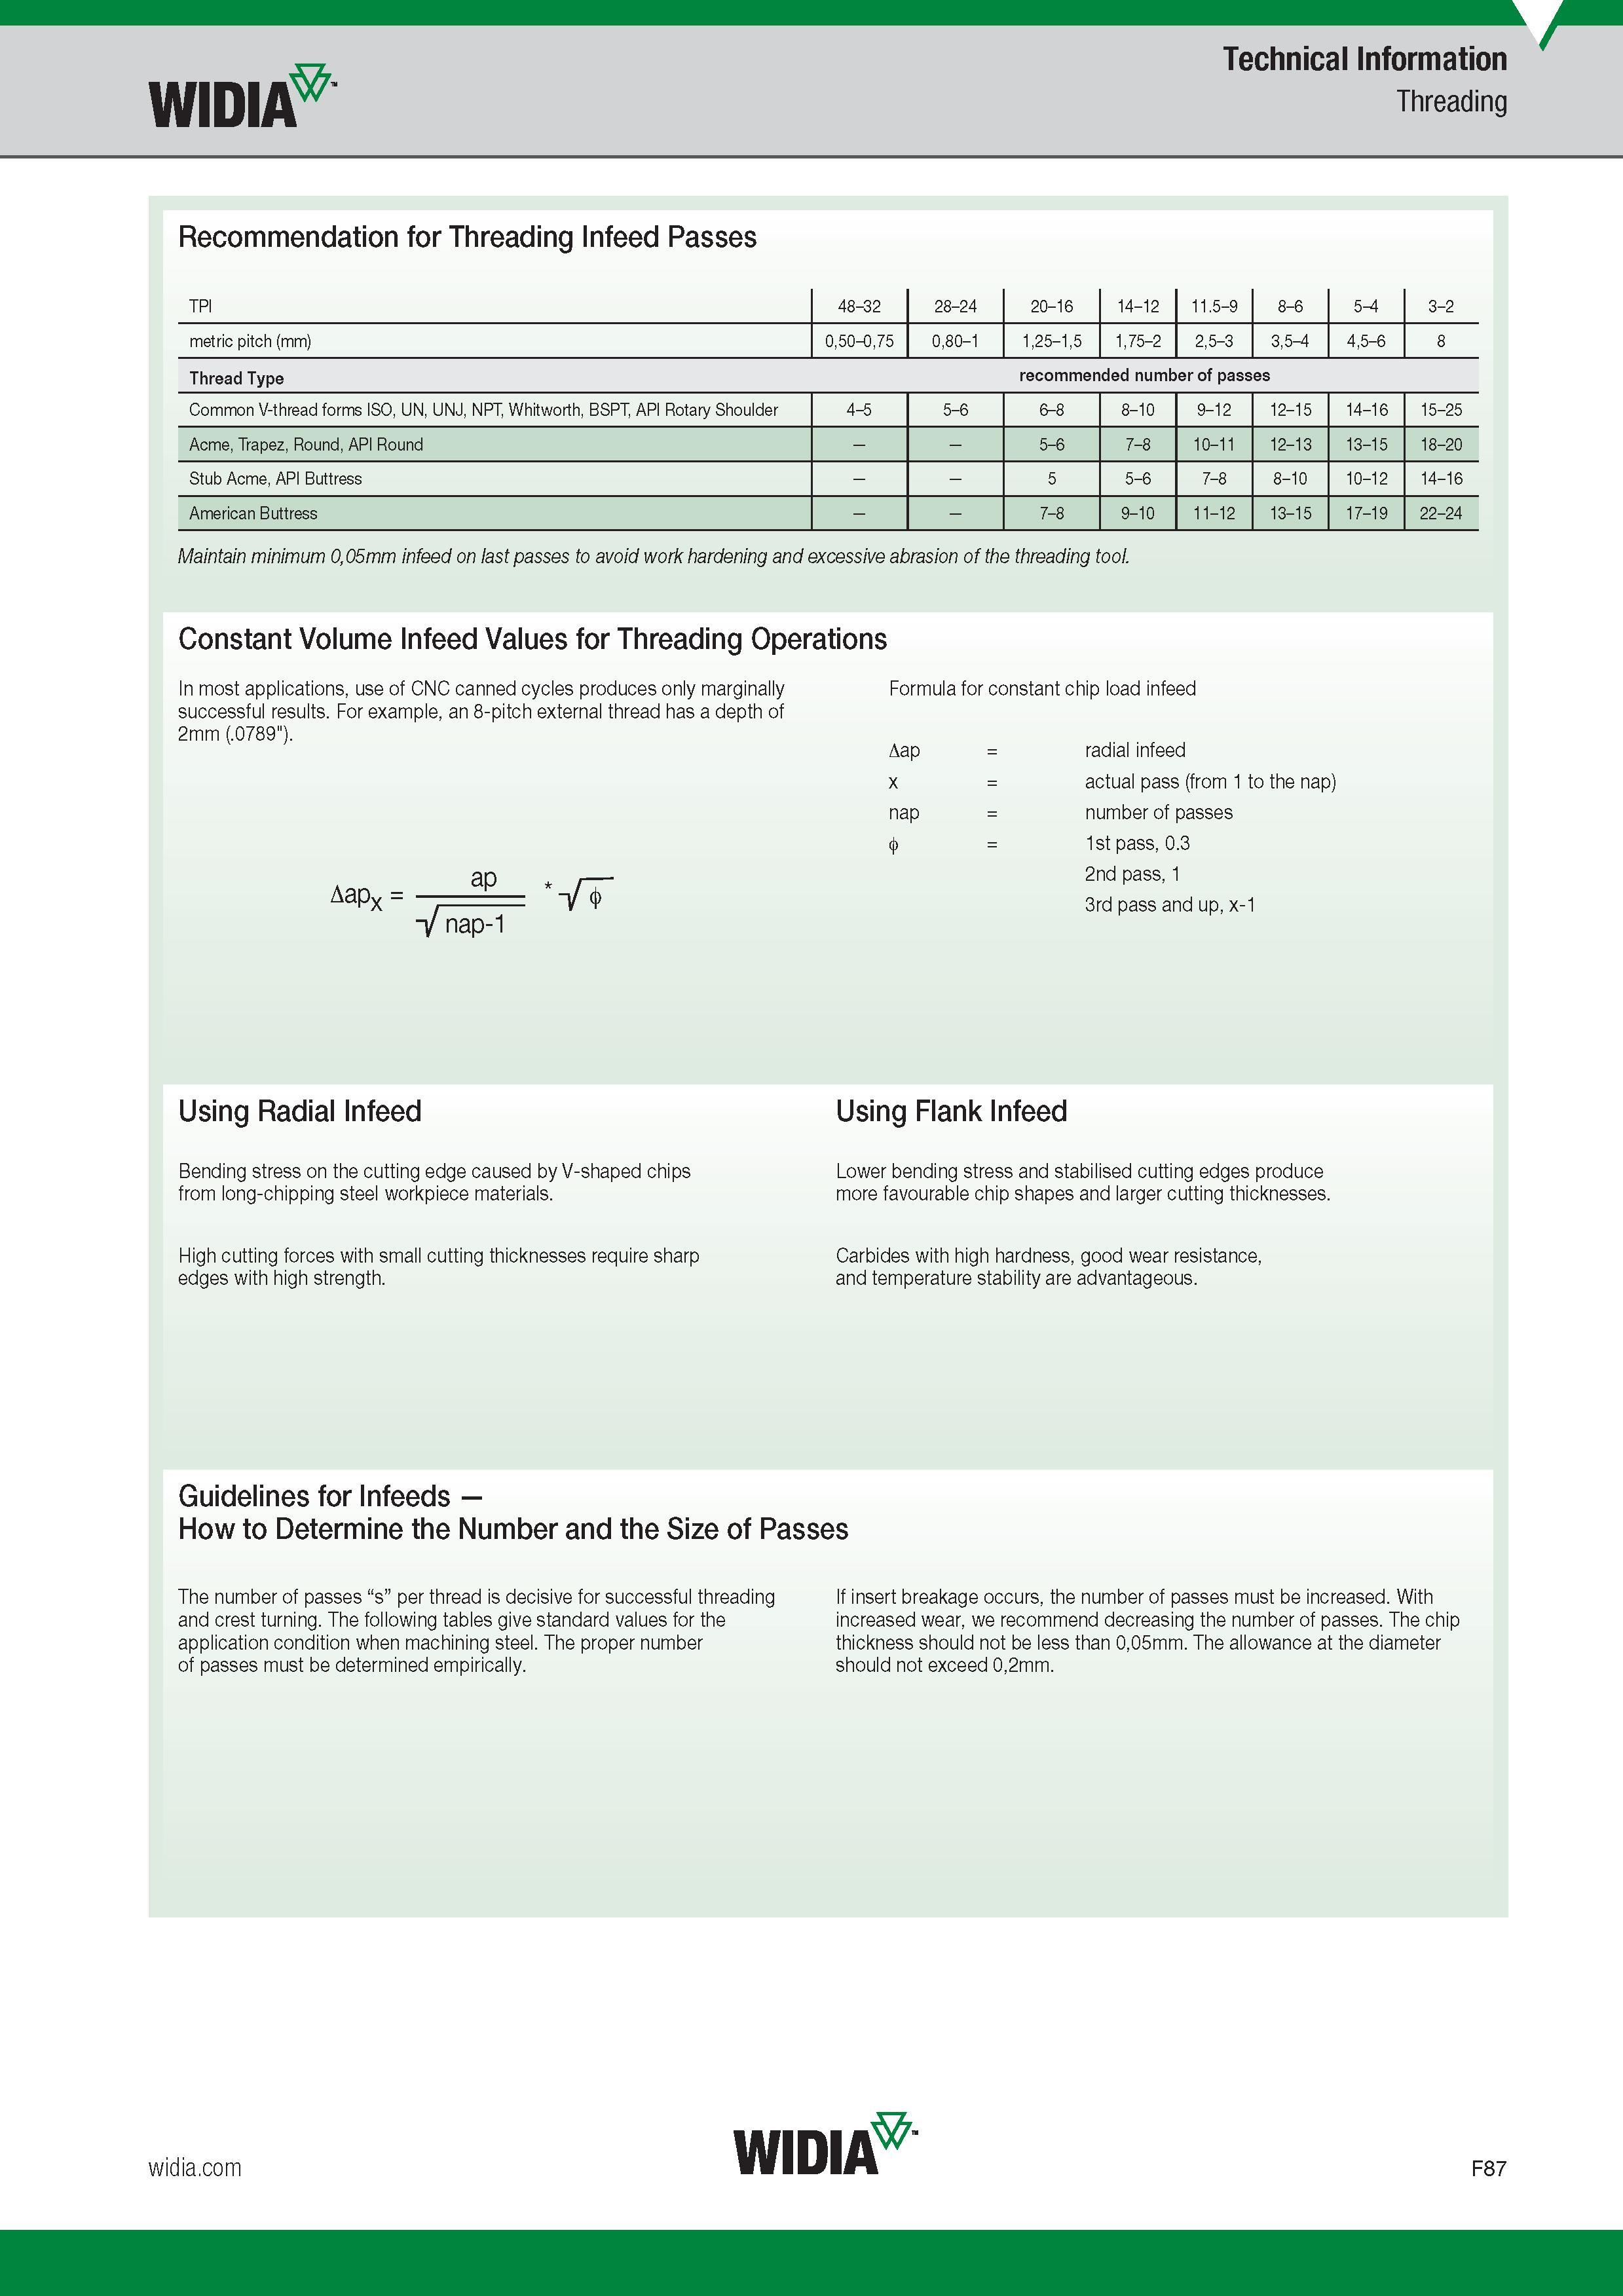
Recommendation for Threading Infeed Passes Maintain minimum 0,05mm infeed on last passes to avoid work hardening and excessive abrasion of the threRecommendation for Threading Infeed Passes Maintain minimum 0,05mm infeed on last passes to avoid work hardening and excessive abrasion of the threading tool. Constant Volume Infeed Values for Threading Operations In most applications, use of CNC canned cycles produces only marginally successful results. For example, an 8-pitch external thread has a depth of 2mm (.0789"). Aapx ap V nap-1 VT Formula for constant chip load infeed Aap radial infeed x actual pass (from 1 nap number of passes 1st pass, 0.3 2nd pass, 1 3rd pass and up, x Using Radial Infeed Bending stress on the cutting edge caused by V-shaped chips from long-chipping steel workpiece materials. High cutting forces with small cutting thicknesses require sharp edges with high strength. Using Flank Infeed Lower bending stress and stabilised cutting edges produce more favourable chip shapes and larger cutting thicknesses. Carbides with high hardness, good wear resistance, and temperature stability are advantageous. Guidelines for Infeeds How to Determine the Number and the Size of Passes The number of passes s per thread is decisive for successful threading and crest turning. The following tables give standard values for the application condition when machining steel. The proper number of passes must be determined empirically. If insert breakage occurs, the number of passes must be increased. With increased wear, we recommend decreasing the number of passes. The chip thickness should not be less than 0,05mm. The allowance at the diameter should not exceed 0,2mm. Technical Information Widia Threading |
|||||
См.также / See also : |
|||||
Соотношение твердостей Таблица / Hardness equivalent table |
Аналоги марок стали / Workpiece material conversion table |
||||
Отклонение размера детали / Fit tolerance table |
Перевод оборотов в скорость / Surface speed to RPM conversion |
||||
Диаметр под резьбу / Tap drill sizes |
Виды резьбы в машиностроении / Thread types and applications |
||||
Дюймы в мм Таблица / Inches to mm Conversion table |
Современные инструментальные материалы / Cutting tool materials |
||||
| |
|||||
| WIDIA | |||||
| |
|||||
 Каталог WIDIA 2017 Металлорежущий инструмент (англ.яз. / ENG) (1972 страницы) |
|||||
 Каталог WIDIA 2018 Инструмент для металлообработки Новинки (106 страниц) |
 Каталог WIDIA 2017 Инструмент токарный для станков (668 страниц) |
 Каталог WIDIA 2017 Инструмент фрезерный монолитный (332 страницы) |
 Каталог WIDIA 2017 Инструмент для обработки отверстий (348 страниц) |
 Каталог WIDIA 2017 Фрезы резьбовые и метчики (122 страницы) |
|
 Каталог WIDIA 2016 Фрезы с режущими сменными пластинами (340 страниц) |
 Каталог WIDIA 2015 Токарный инструмент (382 страницы) |
 Каталог WIDIA 2014 Новый инструмент (422 страницы) |
 Каталог WIDIA 2012 Новый режущий инструмент и оснастка (470 страниц) |
 Каталог WIDIA 2011 Инструментальная оснастка (англ.яз. / ENG) (1190 страниц) |
 Каталог WIDIA 2010 Режущий осевой инструмент (614 страниц) |
| |
|||||
|
Каталоги инструмента и оснастки для металлообработки на станках / Cutting tools and tooling system catalogs |
|||||
| Каталог WIDIA 2017 Металлорежущий инструмент (Всего 1972 стр.) | |||||
| |
|||||
 682 |  683 |  684 |  686 |  687 |  688 |
|
Lab2U | Catalogs | Tap drill sizes | Speed to RPM | Material table Разработчики сайта / Developers of site |
|
Поиск на сайте Lab2u.ru с помощью поисковых систем ЯНДЕКС, BING, GOOGLE:
|
||
|
|
||
